Explore our exciting job openings and become part of the team.

Our proud journey from a handcrafted chimney fan in Sorø to a global market leader with a focus on the green transition.

Dealer portal for existing dealers and partners.

Find your nearest dealer.

Inspiration, tips and tricks for your wood-burning stove and a healthier indoor climate.

CAREER

Your career.
Optimized.

Join Exodraft and our shared
ambition to build the bridge to a CO₂-neutral
future with greener energy for everyone.

How to Choose the Right Composite Part for Your Project?

Choosing the right Composite Part begins with understanding the job, not simply selecting the lightest or strongest material. Each project presents different demands, including load direction, operating temperature, moisture exposure, impact risk, and production volume. A part used inside an aircraft cabin may require different performance from one installed near a marine engine. Context matters.

Performance must be measured against real conditions. Engineers often review fiber type, resin system, laminate orientation, surface finish, and joining methods before approving a design. A carbon fiber component may provide excellent stiffness, while glass fiber can offer practical durability and lower cost. Testing samples under expected loads can reveal weaknesses that specifications overlook. It is also wise to examine dimensional stability, repair procedures, and end-of-life considerations.

Supplier experience remains important. Reliable manufacturers should explain their process controls, inspection methods, material traceability, and relevant quality certifications. Ask for test data, not broad promises. A detailed drawing and clear tolerance requirements can prevent expensive misunderstandings later. Manufacturing capability matters too; an excellent design may fail when produced with inconsistent curing or poor tooling.

No selection method is flawless. An early material estimate can be wrong. That is why experienced teams compare alternatives, consult qualified specialists, and validate prototypes before full production. The best Composite Part is not always the most advanced option. It is the one that delivers dependable performance, practical manufacturability, and acceptable cost throughout the project’s actual service life.
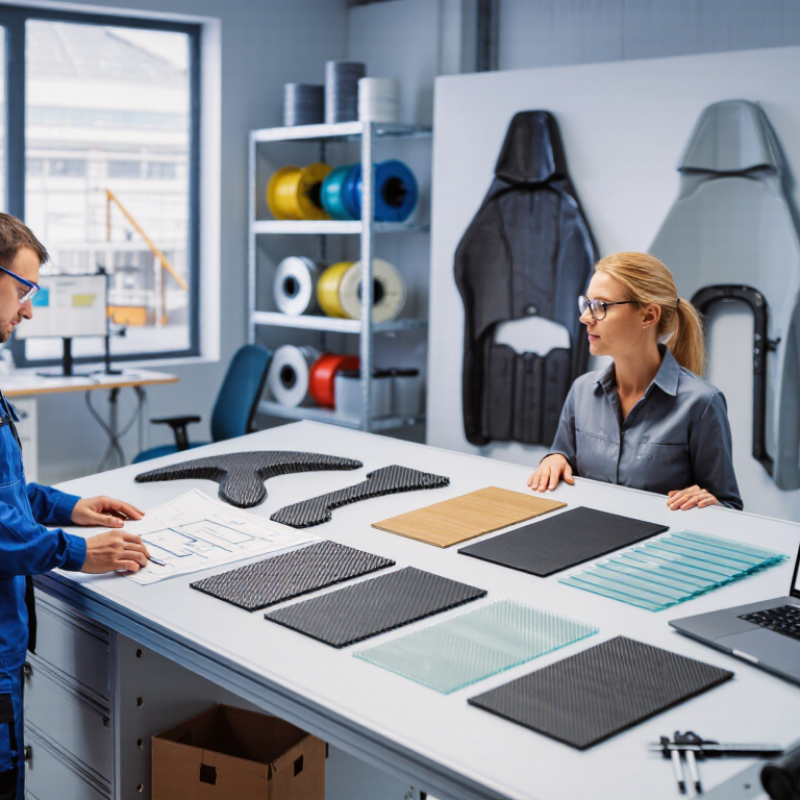
How to Choose the Right Composite Part for Your Project?

Define Project Requirements and Operating Conditions

How to Choose the Right Composite Part for Your Project?

Define Project Requirements and Operating Conditions

Start with the part’s real working environment, not only its drawing. Record load direction, peak force, vibration, temperature, moisture, chemicals, and expected service life. A composite bracket inside a dry machine room faces different risks than one exposed to salt spray and sunlight. NREL’s 2023 Cost of Wind Energy Review uses a 20-year reference life for land-based wind systems. That figure shows why fatigue deserves early attention. A part surviving one overload may still fail after millions of smaller cycles.

Measure the details.

The IEA’s Renewables 2024 report recorded about 510 GW of new renewable capacity in 2023. More outdoor equipment means more composite parts facing weather, thermal cycling, and maintenance demands. Choose fiber orientation and resin performance around those conditions. Check tensile strength, interlaminar strength, moisture absorption, and thermal expansion. ASTM D3039 supports tensile testing, while ASTM D2344 helps assess short-beam interlaminar strength. Ask for test temperatures and conditioning methods, not just headline values. Supplier data can look precise, yet real assemblies often behave differently. Fasteners may crush laminates. Sharp corners may create stress concentrations. I have seen calculations pass while a poorly supported edge failed early. That uncomfortable gap deserves review. Build a prototype, expose it to representative conditions, and inspect it after repeated loading. A smaller safety factor is not automatically efficient. It may simply leave less room for uncertainty.

Compare Composite Materials and Their Performance Properties

Choosing the right composite part starts with service conditions, not material preference. In practice, I record load direction, operating temperature, moisture exposure, impact risk, and expected service life. A lightweight panel may look efficient, yet its stiffness can fall when support spacing is poorly designed. Geometry matters as much as fiber selection. It often decides the result.

Carbon-fiber composites usually provide high stiffness and low weight, making them useful for precise structures and moving components. They can be costly and may fail suddenly under severe impact.

Glass-fiber composites offer good strength, electrical insulation, and cost control. They are heavier, but can tolerate everyday knocks effectively.

Aramid reinforcement is valued for impact and abrasion resistance. However, compression performance and moisture behavior require careful checking. Resin choice also changes temperature resistance, toughness, and production speed. Two parts with identical fibers can perform differently.

I compare supplier test data with the actual load case, then request samples when tolerances are tight. Tests should include fatigue, temperature cycling, water exposure, and fastener behavior. A datasheet alone is not enough.

I once prioritized maximum tensile strength and overlooked edge damage around a mounting hole. That assumption needed correction.

Designers should check repair methods, inspection access, and recycling constraints before approval. In real projects, predictable performance at the mounting hole may matter more than higher headline strength.

Evaluate Part Geometry, Manufacturing Methods, and Tolerances

How to Choose the Right Composite Part for Your Project?

Evaluate Part Geometry, Manufacturing Methods, and Tolerances

Part geometry should guide material selection, not follow it. Deep ribs, sharp corners, and uneven wall thickness can create voids, warping, or difficult demolding. Smooth radii and consistent sections usually reduce manufacturing risk. The U.S. Department of Energy estimates that a 10% vehicle weight reduction can improve fuel economy by 6–8%. That benefit disappears if a lightweight part needs excessive reinforcement or frequent replacement.

Manufacturing methods also shape the final design. Compression molding suits repeatable parts with moderate complexity and stable volumes. Resin transfer molding supports larger structures and controlled fiber placement. Additive manufacturing helps produce prototypes, internal channels, and customized fixtures, but surface finish may require secondary work. The 2024 Wohlers Report valued global additive manufacturing at about 20 billion dollars in 2023. Growth is impressive, but it does not make every printed composite suitable for production.

Tolerances need practical limits. Holding ±0.1 millimeter across a large laminate may increase tooling and inspection costs without improving performance. Define critical dimensions around interfaces, holes, seals, and moving joints. Use datum references and measure parts at controlled temperature. ISO 2768 can support general tolerances, but it cannot replace process capability testing. I have seen designs over-specified early, then weakened during cost reduction. That mistake is avoidable. Build a sample part, record actual variation, and revise the drawing before committing to full production.

How to Choose the Right Composite Part for Your Project? - Evaluate Part Geometry, Manufacturing Methods, and Tolerances

Part Geometry Recommended Manufacturing Methods Common Composite Formats Typical Production Volume Typical Achievable Tolerance Key Design Considerations Best Fit When
Flat panels and simple plates
Constant thickness, limited curvature
Compression molding, prepreg lay-up, vacuum bagging, pultrusion for continuous profiles Glass or carbon fiber with epoxy, polyester, or vinyl ester resin Low to high, depending on tooling and automation Approximately ±0.5 to ±1.5 mm for molded or laminated parts; tighter after machining Control laminate symmetry, fiber orientation, flatness, and resin-rich edges Lightweight covers, structural skins, panels, electrical enclosures, and barriers
Long constant-section profiles
Beams, channels, rods, tubes, and rails
Pultrusion, filament winding for tubes, or continuous lamination Continuous glass or carbon fiber in thermoset resin Medium to very high for repeatable cross-sections Approximately ±0.25 to ±1.0 mm on profile dimensions, depending on size and tooling Maintain constant cross-section; account for die wear, shrinkage, and cut-length variation High-volume structural members requiring consistent stiffness, corrosion resistance, and low weight
Closed hollow cylinders
Pressure vessels, pipes, and tanks
Filament winding, bladder molding, or automated fiber placement Carbon or glass fiber with epoxy or other qualified resin systems Low to high; filament winding scales effectively for repeat production Approximately ±0.5 to ±2.0 mm for diameter; tighter interfaces may require machining Define fiber angles for hoop and axial loads; verify liner, permeability, burst, and fatigue requirements Parts dominated by pressure, torsion, or axial loading and requiring optimized fiber placement
Complex double-curved shells
Fairings, aerodynamic covers, and contoured housings
Prepreg molding, resin transfer molding, vacuum infusion, or automated fiber placement Carbon, glass, or aramid fiber fabrics with epoxy or thermoplastic matrices Low to medium; higher volumes favor matched tooling and automation Approximately ±1.0 to ±3.0 mm before machining, depending on size and mold stability Plan for bridging, wrinkling, spring-in, draft angles, mold access, and consistent surface finish Large, lightweight shells where aerodynamic shape, stiffness, or appearance is important
Thick solid or near-solid sections
Mounts, brackets, blocks, and load-introduction fittings
Compression molding, resin transfer molding, prepreg molding, or machining from composite plate Short-fiber or continuous-fiber composites; glass or carbon fiber systems Low to high, based on tooling investment and required structural performance Approximately ±0.25 to ±1.0 mm for molded features; machined datums can be tighter Avoid abrupt thickness changes; manage voids, exotherm, residual stress, and fastener bearing loads High-load connection points, wear-resistant components, and parts requiring precise interfaces
Parts with ribs, bosses, and integrated details
Housings, brackets, and structural frames
Compression molding, injection molding with short-fiber compounds, or RTM Short-glass-fiber thermoplastics or thermoset molding compounds; continuous inserts where needed Medium to very high for molded thermoplastic or thermoset processes Approximately ±0.2 to ±1.0 mm; dimensional variation increases with wall thickness and fiber loading Use uniform walls, generous radii, appropriate draft, and ribs sized to limit sink and warpage High-volume parts needing integrated features, repeatability, and reduced assembly labor
Highly customized or prototype geometry
Low-volume, frequently revised designs
Hand lay-up, vacuum bagging, additive tooling, CNC machining, or hybrid fabrication Prepreg, woven fabric, unidirectional tape, or machinable composite plate Prototype to low volume Approximately ±1.0 to ±3.0 mm as molded; machined features may achieve approximately ±0.1 to ±0.5 mm Prioritize design flexibility, accessible tooling, repairability, cure control, and inspection of laminate quality Early-stage development, custom equipment, replacement parts, and designs not yet production-released
Planning note: Tolerance ranges are typical preliminary design values, not universal guarantees. Final limits should be confirmed using the selected material system, part size, tooling concept, cure cycle, inspection method, and applicable engineering standards.

Assess Suppliers, Quality Standards, Costs, and Lead Times

Choosing a composite part is less about the lowest quotation and more about measurable supplier discipline. A 2024 MarketsandMarkets report projects the global composites market to reach about USD 126 billion by 2030. Demand is growing, but supplier capability varies widely.

Request evidence of process control, not only attractive samples. ISO 9001 supports documented quality systems, while AS9100 adds stronger controls for aerospace work. Ask for material certificates, fiber orientation records, cure-temperature logs, and inspection results. ASTM and ISO test methods can verify tensile strength, impact resistance, moisture absorption, and dimensional stability. Costs also include tooling, machining, testing, packaging, and rejected parts. A cheaper quote may hide these items. Lead times need equal scrutiny. Confirm raw-material availability, tooling duration, first-article approval, and production capacity. The 2023 Deloitte supply-chain survey reported that many manufacturers still faced significant supply disruption, so a written schedule matters.

Tips: Compare suppliers with one technical checklist. Ask for a sample inspection report. Request realistic, not optimistic, delivery dates. Add contingency time for design changes. My own practical warning is simple: early prototypes often look perfect, yet production exposes voids, warpage, or inconsistent finish. Plan a pilot batch before full release. It costs more initially. It can prevent expensive rework later. Let the supplier explain what could fail, not only what can be delivered.

How to Choose the Right Composite Part for Your Project?

Compare suppliers using four practical procurement dimensions: supplier capability, quality standards, total cost, and lead time.

The chart uses a normalized planning score from 0 to 100. Quality standards include documented process control, traceability, inspection records, and certifications such as ISO 9001 or AS9100 where applicable. Total cost should include tooling, materials, labor, inspection, logistics, and potential rework. Lead-time performance should be verified against the supplier’s documented production schedule and past delivery records.

Select, Test, and Validate the Composite Part for Final Use

How to Choose the Right Composite Part for Your Project?

Select, Test, and Validate the Composite Part for Final Use

Selecting a composite part starts with the load, not the catalogue photograph. Define tension, compression, bending, impact, and fatigue requirements. Record operating temperature, moisture, chemicals, vibration, tolerances, and expected service life. Fiber direction matters greatly. A small alignment error can reduce strength and stiffness. Ask for material data, production records, inspection methods, and lot traceability. A smooth surface proves little.

Test the actual part whenever possible. Begin with dimensional checks and visual inspection under controlled lighting. Look for cracks, delamination, resin-rich areas, and exposed fibers. Use suitable methods to detect hidden defects. Test coupons can measure tensile, compression, flexural, and thermal performance. However, coupons may not represent joints, holes, curved surfaces, or local stress. One good result is not enough. Test several samples under expected and worst-case conditions. Include moisture conditioning, temperature cycling, and repeated loading. Test fixtures can also influence results, so independent review is valuable.

Validation connects laboratory evidence with final use. Install pilot parts in a controlled environment and monitor strain, movement, temperature, and damage. Compare measurements with design predictions and acceptance limits. Keep clear records for each batch and test condition. Recheck the part after manufacturing changes, repairs, or unusual exposure. The process is imperfect. A part can pass testing and still fail through poor installation or overlooked maintenance. That weakness should remain visible in the approval decision. When the consequences are serious, use an accredited laboratory and a qualified engineer to review the evidence.

Contact us

Let us help you with the right solution

Address

HQ
Industrivej 10
5550 Langeskov

Talk to a consultant

Write to us to get in touch with a consultant

Address

HQ
Industrivej 10
5550 Langeskov

Thank you for your inquiry

Be contacted

Questions? Write to us and get a response

Address

HQ
Industrivej 10
5550 Langeskov

Thank you for your inquiry